Bending
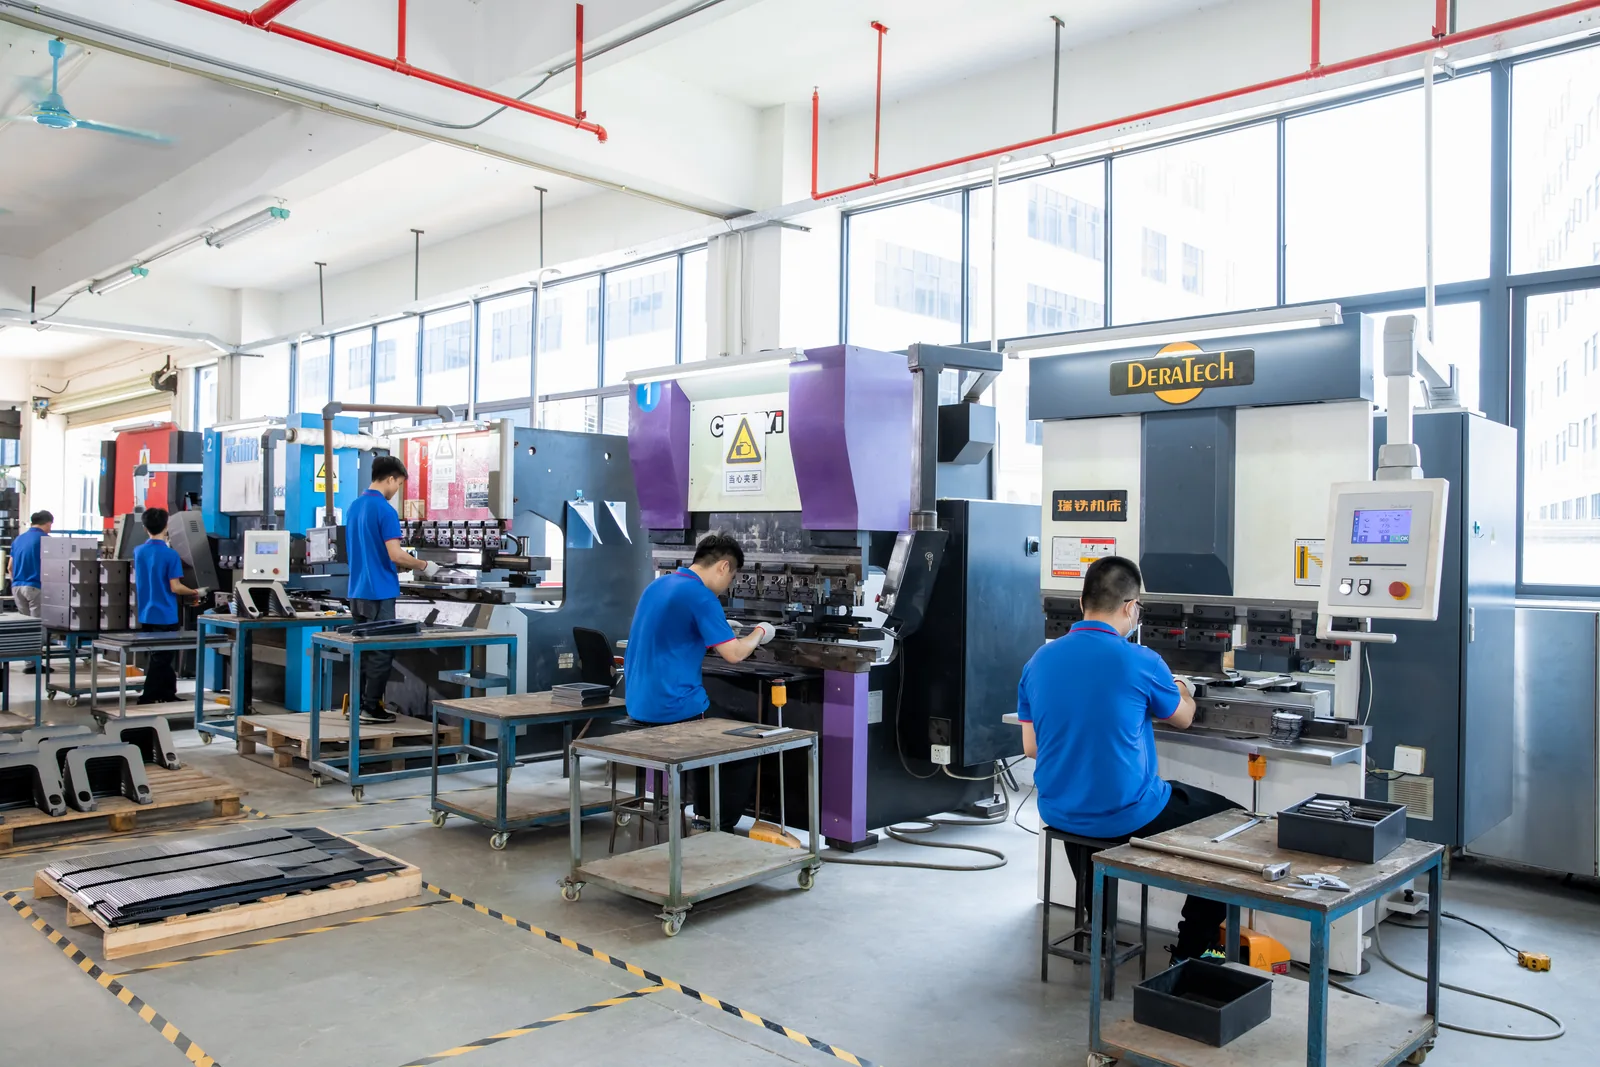
Form sheet parts to the required dimensions and geometry.
Process overview
Plan the bends, forming sequence and critical dimensions around the assembly of equipment housings, cabinets and brackets. Flat blanks become the three-dimensional structures required by the product.
Typical parts
- Equipment cabinets
- Metal housings
- Brackets and mounting plates
Process specifications
- Maximum stated bending length
- 3.2 m
- Equipment rating
- 100 t
- Carbon steel thickness
- Up to 6 mm
- Stainless steel thickness
- Up to 4 mm
Length, tonnage and thickness are separate specifications; their combination depends on the material and geometry.
Discuss your specificationsManufacturing steps
- 01
Review the geometry
Confirm material, bend positions, angles and assembly relationships.
- 02
Agree the sequence
Plan forming operations around the part geometry.
- 03
Form and check
Check critical dimensions against the drawing after bending.
Frequently asked questions
Can a full 3.2 m length of 6 mm carbon steel be bent?
The length, tonnage and thickness values are separate specifications. They do not establish a combined maximum-length, maximum-thickness capability. Please submit the complete drawing for confirmation.
Which dimensions need to be identified?
Identify thickness, bend angles, flange lengths, hole-to-bend distances and critical assembly dimensions.